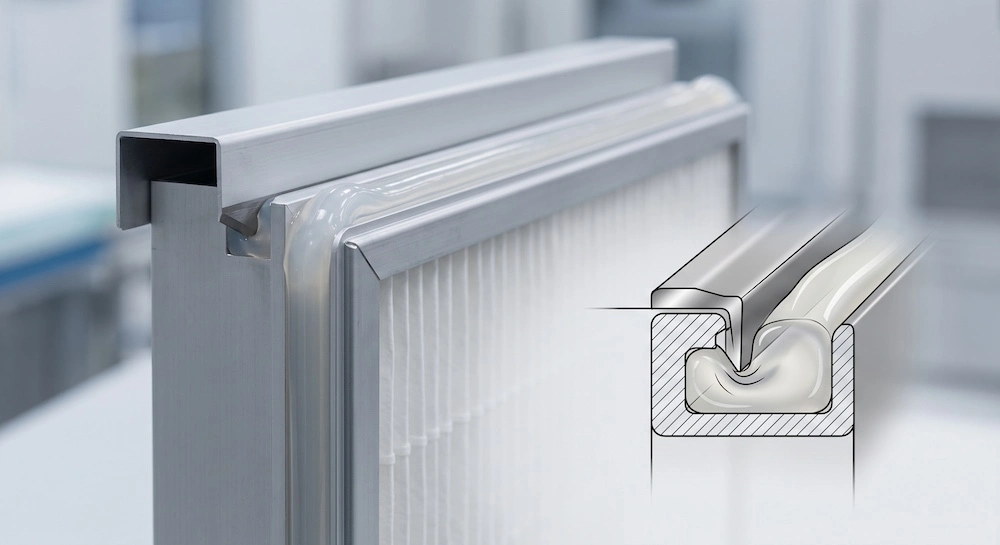

A 610 × 610 mm HEPA filter does not automatically require a fixed amount of silicone gel.
The required quantity depends on the geometry of the sealing channel, the actual gel fill depth, the density of the mixed silicone gel, and the material consumed during production.
For a broader overview of material selection, application and troubleshooting, see our guide to silicone gel for HEPA and ULPA filter sealing.
For a quick estimate:
Silicone gel requirement = Channel volume × Mixed gel density × production allowance
For a simple rectangular sealing channel:
Channel volume = Channel length × Channel width × Actual fill depth
For more complex channels, a better general formula is:
Channel volume = Average cross-sectional area × Effective channel length
This distinction matters because filter dimensions alone do not determine silicone gel consumption. The sealing-channel geometry does.
Quick Answer: How Much Silicone Gel Does a HEPA Filter Need?
There is no universal silicone gel quantity per HEPAFilter.
To calculate it accurately:
- Determine the effective length of the sealing channel.
- Determine its average cross-sectional area.
- Multiply area by length to obtain theoretical gel volume.
- Multiply volume by the density of the mixed A+B silicone gel.
- Add measured production losses when planning actual material requirements.
The general formula is:
V=A×LV=A\times L
Where:
- V = theoretical gel volume
- A = average channel cross-sectional area
- L = effective channel length
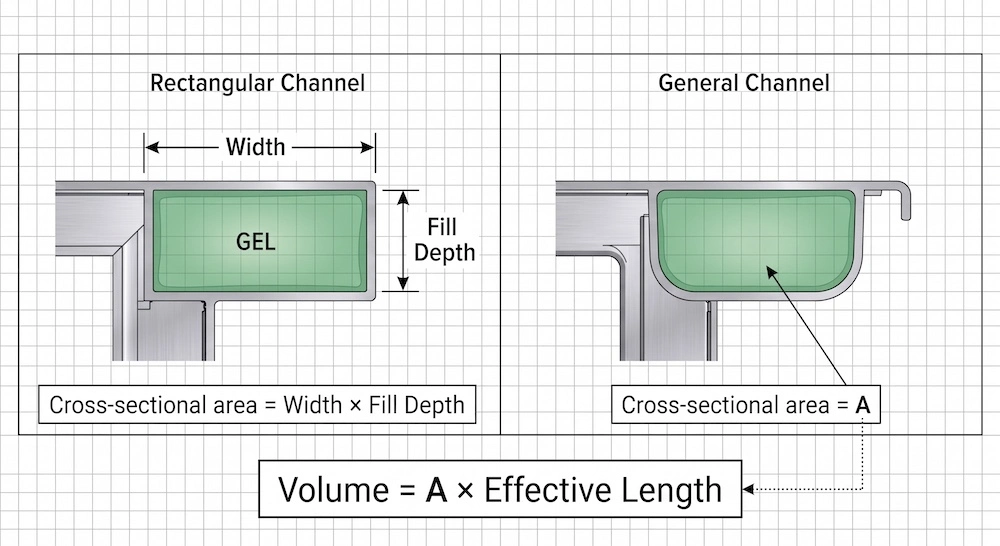
For a rectangular channel:
A=W×FA=W\times F
Therefore:
V=L×W×FV=L\times W\times F
This gives the theoretical volume required to fill the sealing channel. Actual production consumption can be higher because of dispensing losses, equipment residue, start-up material and rejected or reworked filters.
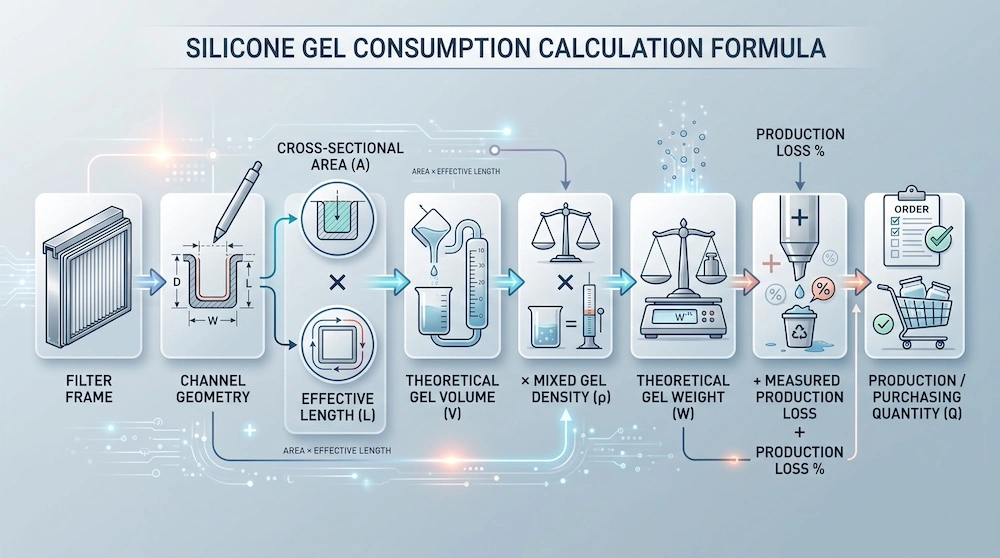
The General Formula for Silicone Gel Consumption
For a simple rectangular channel with dimensions measured in millimeters:
V(cm3)=L(mm)×W(mm)×F(mm)1000V(cm^3)= \frac{L(mm)\times W(mm)\times F(mm)}{1000}
Here, F is the actual fill depth, not necessarily the full physical depth of the channel.
The theoretical gel weight is:
Gel Weight(g)=V(cm3)×Density(g/cm3)Gel\ Weight(g)=V(cm^3)\times Density(g/cm^3)
Therefore:
Gel Weight(g)=L×W×F1000×DensityGel\ Weight(g)= \frac{L\times W\times F}{1000} \times Density
For non-rectangular channels
If the sealing channel has a rounded, U-shaped or otherwise irregular cross-section, first determine its approximate cross-sectional area:
V=A×LV=A\times L
This is more flexible than assuming every filter channel is rectangular.
For production engineering, the objective is to estimate the actual volume occupied by the silicone gel, rather than applying a generic amount based on filter size.
Planning to calculate several filter designs? A future HEPA filter silicone gel consumption calculator can automate this calculation using channel dimensions, density, filter quantity and production loss.
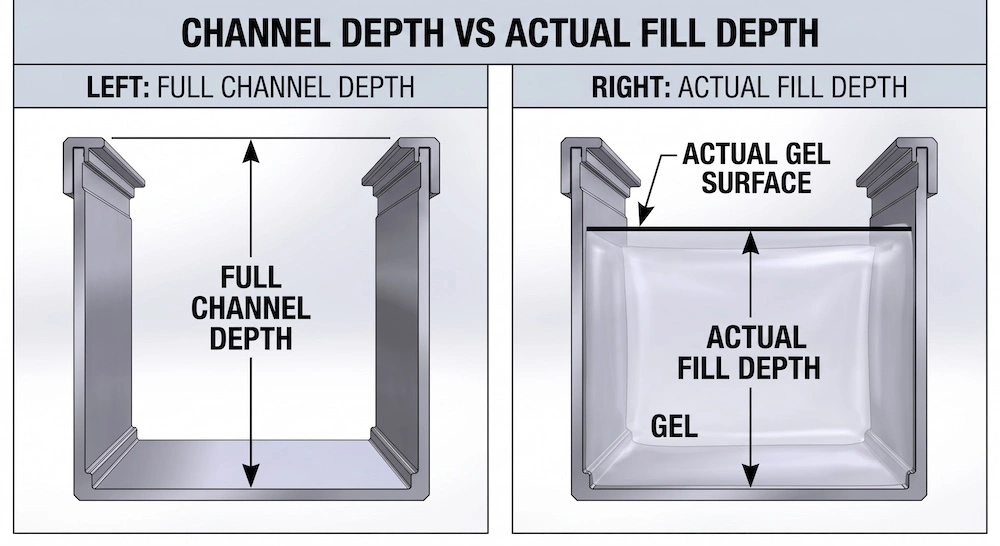
Channel Depth vs. Actual Fill Depth
This is an important distinction that is often overlooked.
Channel depth is the physical depth of the sealing channel.
Actual fill depth is how high the silicone gel actually fills during production.
Zum Beispiel:
- Channel depth: 12 mm
- Actual gel fill depth: 9 mm
If the channel is intentionally not filled to its full depth, the calculation should use 9 mm, not 12 mm.
Using the full channel depth when the actual fill height is lower can significantly overestimate material consumption.
For this reason, production drawings, actual fill-height specifications or measurements from finished filters are preferable to estimating from the frame dimensions alone.
Example 1: Calculate Silicone Gel for One Filter
Suppose an illustrative filter design has:
| Parameter | Example |
| Effective channel length | 2,400 mm |
| Average channel width | 12 mm |
| Actual fill depth | 10 mm |
| Assumed mixed gel density | 1.00 g/cm³ |
The theoretical volume is:
V=2400×12×101000V=\frac{2400\times12\times10}{1000}V=288cm3V=288cm^3
Using the illustrative density of 1.00 g/cm³:
288×1.00=288g288\times1.00=288g
So the theoretical gel requirement is 288 g per filter.
If an illustrative 10% production allowance is applied:
288×1.10=316.8g288\times1.10=316.8g
The planning quantity would therefore be approximately:
317 g per filter
The 10% figure is used only to demonstrate the calculation. It should nicht be treated as a universal production-loss standard. Actual production loss should be established from the dispensing process.
For an actual material evaluation, use the mixed-system density stated in the current supplier TDS.
Why Filter Size Alone Is Not Enough
A common question is:
“How much silicone gel does a 610 × 610 mm HEPA filter need?”
The answer cannot be determined from 610 × 610 mm alone.
Two filters with the same face dimensions can have different:
- Frame thicknesses
- Channel lengths
- Channel widths
- Channel depths
- Knife-edge designs
- Fill heights
- Corner geometries
Consequently, their silicone gel consumption can be different.
The key rule is:
Filter dimensions determine the overall filter size; sealing-channel geometry determines silicone gel consumption.
Gel-seal filter systems commonly use a perimeter gel track that interfaces with a housing knife edge. The actual sealing geometry therefore matters when evaluating the required sealing material.
For a technical reference on gel-seal and knife-edge configurations, see the MANN+HUMMEL Gel Seal Identification Guide.
Example 2: How Much Gel for 500 Filters?
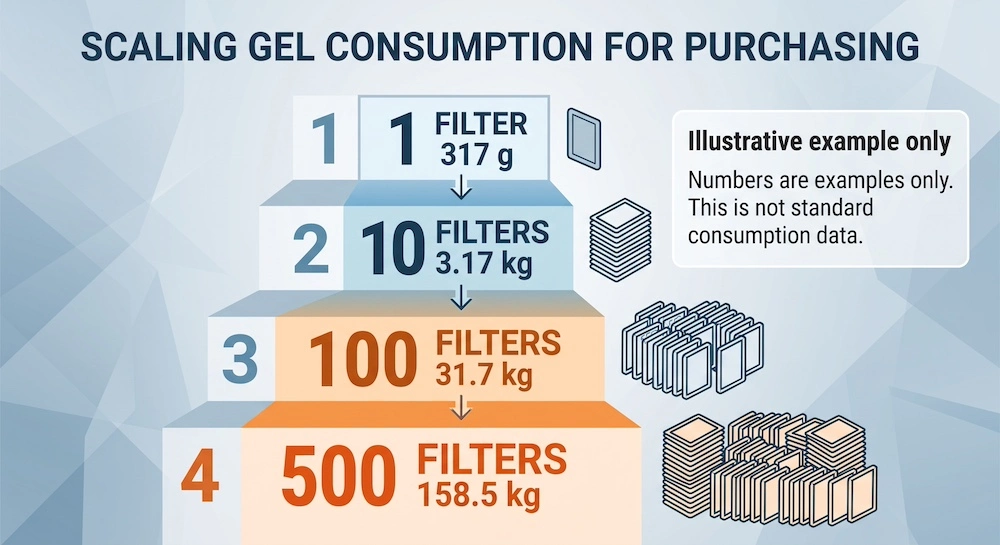
Assume the previous example gives an estimated production requirement of:
317 g/filter
For 500 filters:
317×500=158,500g317\times500=158,500g
or:
158.5kg158.5kg
Therefore, approximately 158.5 kg would be required under this illustrative assumption.
However, this number should not automatically become the final purchase quantity.
You should also consider:
- Mixer residue
- Hose residue
- Static or dynamic mixer waste
- Equipment priming
- Start-up material
- Dispensing variation
- Rejected filters
- Rework
- Packaging and batch constraints
Therefore, the final purchasing quantity should be based on validated production consumption, not simply the theoretical channel volume.
The Four Numbers You Should Not Confuse
A useful way to manage silicone gel consumption is to separate four different quantities.
| Quantity | What it means | Main use |
| Theoretical quantity | Gel needed to occupy the calculated channel volume | Engineering calculation |
| Net sealing quantity | Gel actually deposited into the sealing channel | Process optimization |
| Production consumption | Total material consumed to produce good filters | Production planning |
| Purchasing quantity | Material that should be ordered | Procurement |
This distinction is critical.
For example, a filter may theoretically require 288 g of gel, but the production line may consume 315 g per good filter because of equipment residue and start-up waste.
Therefore:
Theoretical consumption is not necessarily the same as production consumption or purchasing quantity.
How to Measure Actual Silicone Gel Consumption
Once production begins, actual consumption can be measured rather than estimated.
For example, suppose a production run starts with:
5.2 kg of silicone gel
After producing 10 filters, 2.0 kg remains.
Total material consumed:
5.2−2.0=3.2kg5.2-2.0=3.2kg
Average production consumption:
3.2kg÷10=320g/filter3.2kg\div10=320g/filter
This gives:
320 g of production consumption per filter
However, this number may include material remaining in the mixer, hoses or dispensing system.
For process optimization, it is useful to separately record:
- Material loaded into the equipment
- Material actually dispensed
- Material remaining in equipment
- Material deposited into the channel
- Number of good filters produced
This helps distinguish sealing consumption from process loss.
How Much Production Loss Should You Allow?
There is no single loss percentage that applies to every HEPA filter production line.
The actual loss depends on:
- Manual or automatic dispensing
- Mixer design
- Hose length
- Static mixer configuration
- Priming procedure
- Start-up procedure
- Operator technique
- Filter rejection rate
- Material remaining in equipment
A percentage such as 5% or 10% can be used as an illustrative planning assumption, but it should not be presented as an industry standard.
For an established production line, the better method is:
Loss Factor=Production Consumption−Net Sealing QuantityNet Sealing QuantityLoss\ Factor= \frac{Production\ Consumption-Net\ Sealing\ Quantity} {Net\ Sealing\ Quantity}
This allows the manufacturer to establish a loss factor based on its own equipment and process.
5 Common Mistakes When Calculating Silicone Gel Consumption
- Using filter face dimensions
A 610 × 610 mm filter does not automatically have a specific gel requirement.
Use the sealing-channel geometry.
- Using full channel depth instead of actual fill depth
If the channel is 12 mm deep but only 9 mm is filled, use the actual 9 mm fill depth.
- Using the wrong density
The density used for weight conversion should correspond to the mixed silicone gel system being evaluated.
Do not automatically use the density of Part A or Part B alone.
- Treating theoretical quantity as purchasing quantity
Theoretical channel volume does not include mixer residue, priming, start-up waste or rejected filters.
- Applying a fixed industry loss percentage
There is no universal production-loss percentage for every filter manufacturer.
Measure the actual process whenever possible.
How to Estimate Silicone Gel for a Trial Order
For a new filter design, the most reliable approach is to work through three stages.
Stage 1 — Engineering estimate
Use:
- Channel length
- Cross-sectional area
- Actual fill depth
- Mixed gel density
This gives the theoretical requirement.
Stage 2 — Controlled production trial
Produce a known number of filters and record:
- Material loaded
- Material dispensed
- Material remaining
- Good filters produced
- Rejected or reworked filters
Stage 3 — Establish actual consumption
Calculate:
Actual Production Consumption=Total Material Used÷Good FiltersActual\ Production\ Consumption= Total\ Material\ Used \div Good\ Filters
This number can then be used for future purchasing and production-cost calculations.
If you are evaluating silicone as an alternative to polyurethane, see our detailed comparison of silicone gel vs polyurethane gel for HEPAFilter sealing before finalizing the material trial.
What Information Is Needed to Estimate Your Gel Consumption?
You do not always need a complete engineering drawing.
For an initial estimate, any of the following can be useful:
Best option
Filter-frame drawing with channel dimensions
Also useful
- Channel length
- Channel width
- Channel depth
- Actual fill height
- Cross-sectional drawing
- Photo with dimensions marked
- Current gel consumption per filter
If you are replacing an existing polyurethane or silicone gel, your current consumption per filter can also provide a useful reference for planning a trial.
For more information about the material itself, see TP-012 silicone gel for air filter sealing.
Need a Silicone Gel Consumption Estimate?
Topsil Silicone can help estimate the required material quantity for a new HEPA or ULPA filter sealing project.
Send us any available information, such as:
- Filter-frame drawing
- Gel-channel dimensions
- Actual fill depth
- Number of filters
- Current sealing material
- Current consumption per filter
- Manual or automatic dispensing method
We can help estimate:
Theoretical gel volume → gel weight → estimated production requirement → trial quantity
Don’t have a channel drawing?
Send us a photo of the filter frame with the key dimensions marked. That can be enough for an initial calculation.