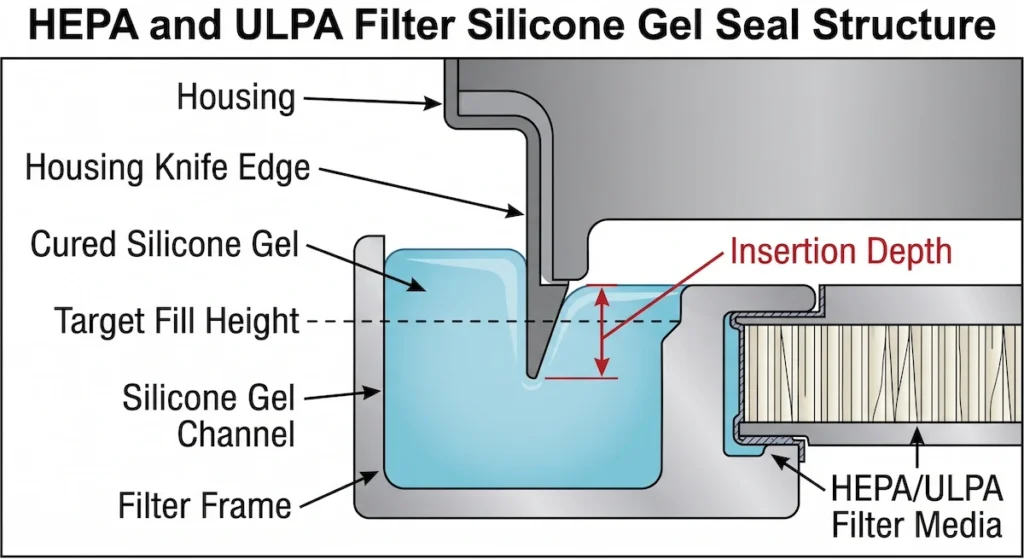

A filter can use high-efficiency media and still fail at the filter-to-housing interface. If the gel channel is underfilled, the silicone is incompletely cured, the knife edge is damaged, or the frame and housing do not match, unfiltered air may bypass the media.
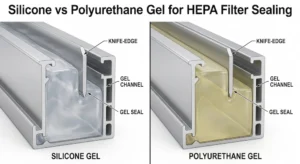
Silicone gel for a gel-seal HEPA or ULPA filter is normally dispensed into a perimeter channel and cured into a soft, tacky material. During installation, the housing knife edge penetrates the gel and creates a conforming barrier. The right material must match the channel geometry, dispensing equipment, production cycle, operating environment and finished-filter qualification plan.
Respuesta rápida
Do not select a HEPA filter silicone gel by softness or cure time alone. Use the production condition to identify the property and test that matter most:
| If your condition is… | Prioritize… | Verify by… |
| Narrow or complex gel channel | Flow, leveling and air release | Trial dispensing in the actual channel |
| Long hose or static mixer | Working time and A/B output stability | Timed ratio checks at production flow |
| Thick knife edge or deep insertion | Softness, insertion force and tear resistance | Representative insertion-and-removal test |
| Painted or adhesive-contaminated frame | Cure compatibility | Clean-cup control plus surface-contact tests |
| Short production cycle | Handling cure, not only full cure | Move/stack/inspect trial at defined intervals |
| Pharmaceutical or cleanroom use | Migration, aging and documentation | Application-specific exposure and finished-filter tests |
How a HEPA/ULPA Gel Seal Works
A gel-seal filter has a continuous perimeter channel. The manufacturer fills it with mixed gel and cures the frame level. During installation, the housing knife edge enters the gel.
The seal succeeds when the gel surrounds the knife edge without leaving a bypass path. Four elements work together:
- Gel: softness, cohesive strength, tack, recovery and long-term stability;
- Channel: width, depth, continuity, corner geometry and fill level;
- Knife edge: thickness, straightness, surface condition and insertion depth;
- Housing and installation: alignment, flatness, mechanical support and operating conditions.
“Self-healing” does not mean unlimited or instantaneous repair. A useful test defines the knife-edge dimensions, insertion depth, number of cycles and recovery time, then checks whether a persistent channel, tear or displaced gel remains.
The gel controls the filter-to-housing interface; HEPA/ULPA classification and integrity remain finished-filter requirements.
When Does a Gel Seal Make Sense?
Gel seals are commonly used in terminal HEPA/ULPA filters, fan filter units and cleanroom ceiling systems whose housings already have compatible knife edges. Typical environments include pharmaceutical manufacturing, laboratories, healthcare, biotechnology and microelectronics.
Choose from the housing outward. A gasket-compression housing may need mechanical redesign before conversion to gel; a knife-edge system requires the gel, channel and blade to be qualified together.
The later supplier-information checklist consolidates the drawings, dimensions, process conditions and qualification data needed for a material review.
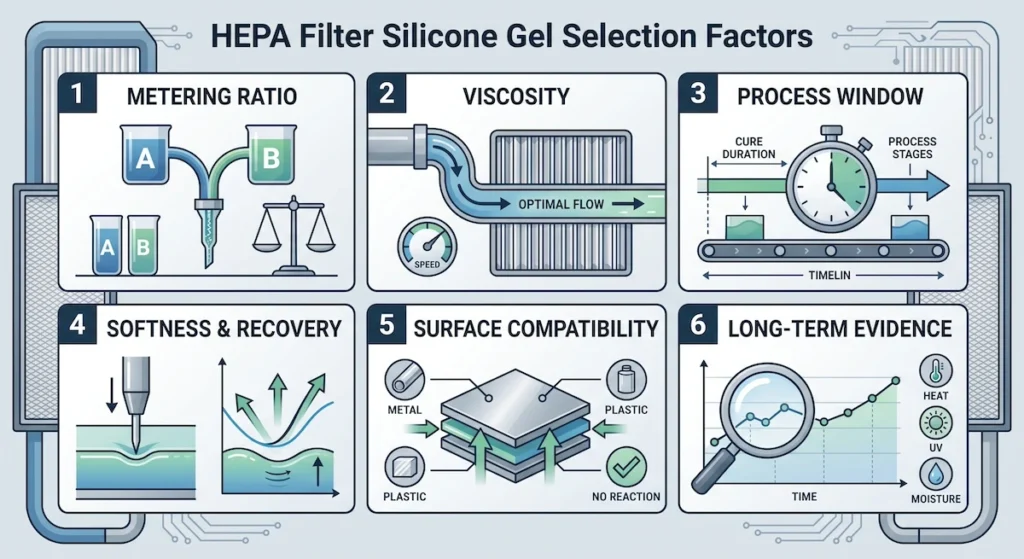
How to Select the Silicone Gel
- Match the Mixing Ratio to the Equipment
A 1:1 gel can simplify metering, but the ratio must be defined by weight, volume, or both; these are not equivalent when component densities differ.
Decision rule: For automatic production, check timed A/B outputs at start-up, normal and low flow. Correct ratio drift before judging the gel.
- Select Viscosity for the Channel and Process
Lower viscosity can improve leveling and air release; higher viscosity may give more fill control. Pump capacity, hose length, mixer pressure drop and temperature also matter.
Decision rule: If bubbles concentrate at corners, first adjust the nozzle path, filling direction and flow. Lower viscosity may otherwise create overflow without removing the air source.
- Separate Working Time, Handling Cure and Full Cure
- Working time: how long the mixed gel remains reliably processable;
- Handling cure: when the filter can be moved or stacked without disturbing the fill;
- Full cure: when the specified properties are reached under stated conditions.
Decision rule: If filters move after four hours, a “24-hour full cure” value is insufficient. Ask for handling-cure data at actual temperature and channel depth.
- Balance Softness With Cohesive Strength
A softer gel usually reduces knife-edge insertion force, but the softest grade is not automatically the safest. The gel must remain stable in the channel, resist unacceptable tearing and recover after the expected insertion cycle.
Compare softness only when suppliers use the same method and conditions. Penetration, Shore 00 and internal compression results are not interchangeable.
Decision rule: If insertion is difficult without gel tearing, check cure and geometry before requesting a softer grade. Softness cannot correct excessive insertion depth or frame distortion.
- Test Cure Compatibility on Every Contact Surface
Addition-cure silicone can be inhibited by certain sulfur compounds, amines, organotin compounds, plasticizers, release agents, coatings and uncured neighboring materials. A clean mixing cup may cure normally while gel touching the frame remains wet.
Decision rule: If the cup cures but the frame-contact sample does not, keep the correct ratio and test the coating, corner adhesive, cleaner and adjacent materials separately.
- Demand Evidence for Aging and Migration Claims
Color and initial softness do not prove long-term cleanliness. Ask what was measured, for how long, at what temperature and after which chemical exposure. Camfil has reported historical cases in which low-molecular-weight fluid migration was associated with gel-seal problems. The report does not mean every silicone gel will fail, but it shows why formulation-specific evidence matters. See the original Camfil gel-seal discussion.
Match the Mixing Ratio to the Equipment
A 1:1 gel can simplify metering, but the ratio must be defined by weight, volume, or both; these are not equivalent when component densities differ.
Decision rule: For automatic production, check timed A/B outputs at start-up, normal and low flow. Correct ratio drift before judging the gel.
Silicone Gel vs Polyurethane Gel vs Gasket Seal
These are screening factors; actual results depend on the formulation and system.
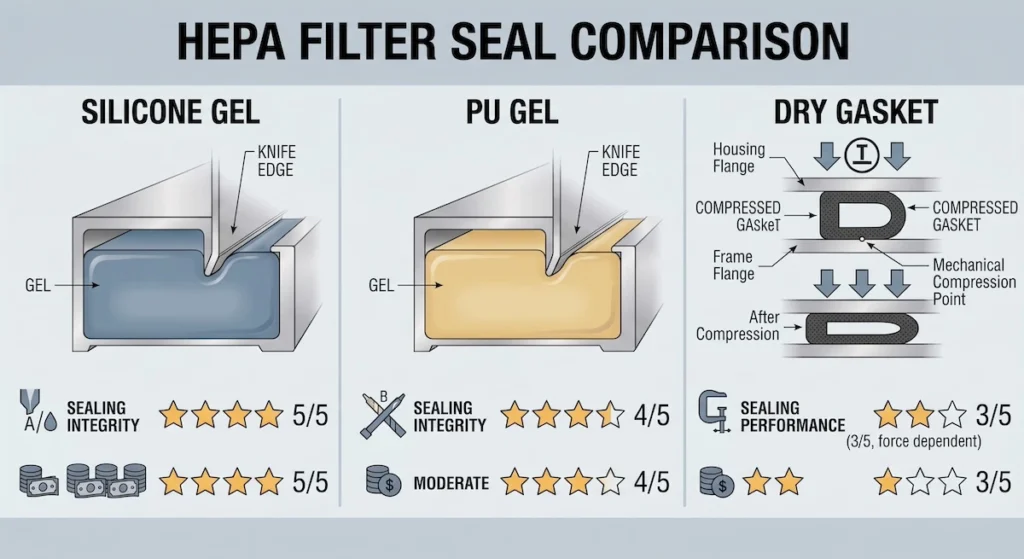
| Decision factor | Silicone gel | Polyurethane gel | Dry gasket |
| Housing requirement | Knife-edge gel channel | Knife-edge gel channel | Controlled compression surface |
| Factory processing | A/B metering, mixing, filling and cure | A/B metering, mixing, filling and cure | Gasket placement; no channel cure |
| Temperature behavior | Broad flexibility is possible; verify the grade | Highly formulation-dependent | Depends on gasket polymer and compression set |
| Moisture/chemical exposure | Verify migration, swelling and chemical compatibility | Verify moisture sensitivity, hydrolysis and chemical compatibility | Verify swelling, hardening and compression retention |
| Repeated installation | Recovery and cohesive strength must be tested | Recovery and cohesive strength must be tested | Compression set and surface damage must be tested |
| Cost comparison | Include material, equipment, scrap and cycle time | Include material, equipment, scrap and cycle time | Include gasket fabrication, installation labor and clamping design |
| Main qualification question | Will the cured gel remain clean, stable and recoverable? | Will the PU remain stable under the actual environment? | Will compression remain uniform over the complete perimeter? |
The best option passes the required test in the intended housing and runs consistently. AAF likewise presents fluid/gel and dry/gasket seals as different configurations.
How Much Silicone Gel Does a Filter Need?
A common sample-planning error is using only the outer filter size. Identical outer dimensions can hide different channels, fill heights and losses.
For an approximately rectangular channel, when length is entered in metres and width/depth in millimetres:
Net volume (cm³) = channel centerline length (m) × internal width (mm) × target fill depth (mm)
Net mass (kg) = net volume (cm³) × verified mixed density (g/cm³) ÷ 1,000
Trial quantity (kg) = net mass per filter × filter quantity × (1 + documented loss %) + equipment-priming quantity
Illustrative Example—not a Standard 610 × 610 mm Filter
Assume the measured channel centerline is 2.4 m, internal width is 12 mm and target fill depth is 10 mm:
- Net volume: 2.4 × 12 × 10 = 288 cm³
- At an illustrative mixed density of 1.00 g/cm³: 0.288 kg per filter
- Ten filters: 2.88 kg net
- If the factory has documented 10% filling loss: 3.17 kg, plus hose and mixer priming
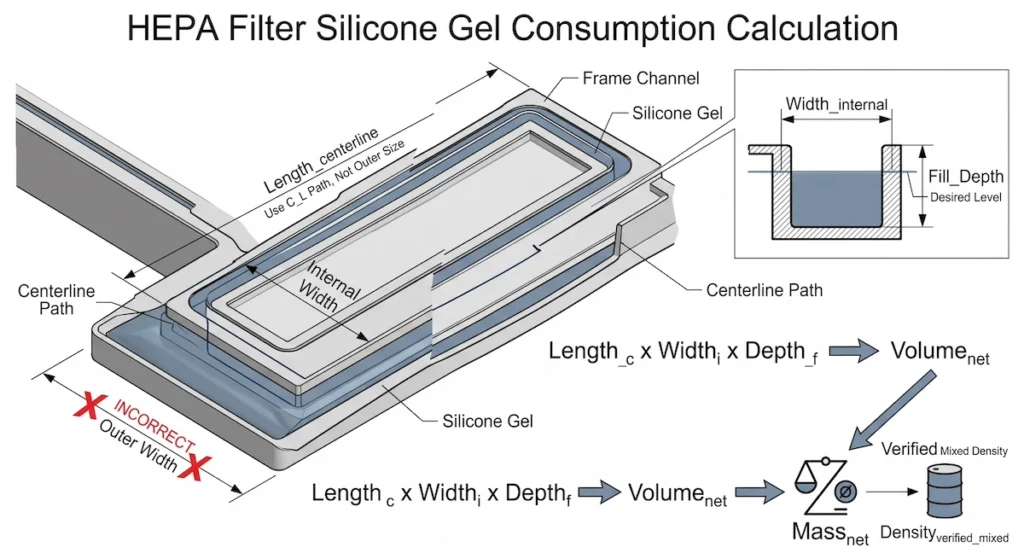
Use the actual channel drawing and approved density; none of the example values is a recommendation.
Topsil application note: In short trials, equipment set-up can consume more material per filter than normal production. A request for “enough gel for ten filters” therefore needs the channel dimensions, number of filter variants, hose/mixer volume and expected start-up adjustments.
Calculate a practical trial quantity: Send the channel centerline length, width, fill height, filter quantity and dispensing method to Topsil.
Mixing and Dispensing: Control the Process Before Blaming the Gel
| Process stage | Control | Record |
| Material conditioning | Bring both components to the approved processing temperature | Material and room temperature |
| Metering | Verify the correct ratio at actual flow | A/B timed output or weight check |
| Mezcla | Blend completely without avoidable air | Mixer type, batch size and mix time |
| Degassing | Use only when the trial shows it is needed | Vacuum level/time or no-degas basis |
| Dispensing | Fill continuously; avoid trapping air at corners | Flow rate, nozzle path and mass per filter |
| Cura | Keep frames level and protected | Handling time, full cure and inspection time |
For manual trials, measure accurately and scrape the container. In production, evaluate the mixer during start-up, normal flow and pauses; initial output may not represent stable production.
Use bottom-up filling and a consistent nozzle path. Random fine bubbles suggest air entrainment; repeated corner voids suggest filling direction or geometry.
Topsil TP-012 silicone gel for HEPA filter sealing is a pourable, addition-cure system available in clear or blue. Published starting values include a 1:1 ratio, 20–30 minute working time and 12–24 hour room-temperature cure; confirm the latest TDS and validate them under production conditions.
When TP-012 May—or May Not—Fit the Project
TP-012 May Be a Suitable Trial Candidate When:
- the line can process the published TP-012 ratio and cure chemistry;
- a pourable clear or blue gel is required;
- the production cycle can accommodate the validated working and cure window;
- the filter uses a compatible gel channel and knife-edge housing;
- the manufacturer will qualify the gel on actual frames before mass production.
Additional Technical Review Is Required When:
- the installed equipment cannot deliver the specified ratio;
- the process requires very rapid heat cure or immediate stacking;
- the seal will face unusual temperature, disinfectant or aerosol exposure;
- the specification includes defined migration, PAO/DOP, flame or insertion-cycle requirements;
- the frame coating or adjacent adhesive has not been checked for cure inhibition.
This distinction prevents a TDS match from being mistaken for application approval.
This distinction prevents a TDS match from being mistaken for application approval.
A Production Trial Needs Pass/Fail Criteria
A cup test confirms that A and B react; production approval requires the actual frame, dispensing method, representative housing and pre-agreed criteria.
| Trial item | What to record | Pass/fail criterion to define |
| Clean-cup cure | Ratio, mass, temperatures and cure time | Uniform cure at the specified checkpoint |
| Frame-contact cure | Coating, adhesive and cleaning process | No uncured interface or local soft area |
| Fill quality | Mass, fill height, corners and bubbles | Approved visual and dimensional limits |
| Process repeatability | Mass of each pilot filter | Maximum acceptable variation |
| Handling cure | Time before moving or stacking | No surface displacement or permanent deformation |
| Knife-edge insertion | Blade dimensions, depth and force | No unacceptable overflow, tear or frame distortion |
| Recovery | Removal cycles and inspection time | No continuous residual path after the defined recovery period |
| Finished-filter integrity | Applicable method and conditions | Customer/project acceptance limit |
| Aging/compatibility | Temperature, humidity, chemicals and duration | Defined change limits for appearance and seal behavior |
Use enough pilot filters to observe variation. Record consumption and set-up loss for the next run.
Troubleshooting by Diagnostic Branch
Branch 1: The Gel Does Not Cure Even in a Clean Cup
Check A/B ratio, component delivery, mixing, batch, shelf life and temperature. Repeat with clean tools; if it still fails, stop and investigate the material or metering system.
Branch 2: The Cup Cures, but Gel Touching the Frame Does Not
Suspect contact inhibition. Test the bare frame, coating, adhesive, label, cleaner and nearby sealant separately. Do not hide the cause by changing the ratio.
Branch 3: The Gel Cures, but Bubbles or Uneven Fill Remain
Map the defects. Distributed bubbles point to mixing or degassing; repeated corner voids point to nozzle path or flow. A sloped surface calls for a level check before a viscosity change.
Branch 4: The Gel Looks Correct, but the Finished Filter Leaks
Locate the leak first. Inspect underfill, knife-edge continuity, insertion depth, frame distortion, housing welds, media and frame adhesive. Another interface may provide the bypass path.
| Symptom | High-priority check |
| Difficult insertion | Cure condition, gel softness, blade thickness and insertion depth |
| Overflow during installation | Fill mass and knife-edge displacement volume |
| Tear after removal | Insertion depth, edge damage, gel strength and cycle count |
| Oil or residue | Contamination source, adjacent materials and migration/aging evidence |
| Batch-to-batch cure change | Temperature, metering, stored components and COA data |
Standards, Certifications and Claims: Keep Them Separate
The raw gel, completed filter and cleanroom system are different qualification levels.
- The gel supplier should provide grade-specific TDS, SDS, quality and applicable compliance documents.
- The filter manufacturer controls channel filling, cure, assembly and completed-filter testing.
- The cleanroom owner or system provider controls installation and site qualification.
Do not state that a raw silicone gel is “EN 1822 certified” merely because it is used in a filter tested to EN 1822 or ISO 29463. A flame, PAO/DOP or migration claim should identify the product, specimen, method and conditions; otherwise, require application testing.
What to Send the Silicone Gel Supplier
To receive a useful recommendation and sample quantity, provide:
- filter type, dimensions and intended environment;
- channel centerline length, width, depth and target fill height;
- knife-edge dimensions and insertion depth;
- frame material, coating and adjacent adhesives;
- manual or automatic dispensing details;
- required working, handling and full-cure times;
- production and service temperatures;
- chemical, humidity or aerosol exposure;
- pilot-filter quantity and annual demand;
- current gel TDS, if replacing another material;
- finished-filter test method and acceptance criteria.
Preguntas frecuentes
Ensure “Zero-Leak” HEPA/ULPA Filters—Starting with the Right Gel
Struggling with incomplete curing, bubbles, or gel overflow? Contact us today with your channel dimensions and process parameters. Topsil’s expert team will provide tailored selection advice, precise trial volume calculations, and a TP-012 silicone gel test sample.